M12 Connector Supplier Criteria for Reliable Industrial Connectivity
2026-11-16
Industrial networks live or die by connections that are easy to overlook. An M12 connector failing on a vibrating packaging line or a wet food-processing floor isn't a small nuisance—it's unplanned downtime, scrambled diagnostics, and a service call nobody budgeted for. Choosing the right supplier is less about catalog specs and more about knowing which criteria actually predict that kind of reliability. From contact design and shielding to materials that survive real washdowns, the gap between 'compatible' and 'dependable' is wider than it looks. Brands like REUNION have carved out a reputation by addressing those field-level failures before they reach your cabinet. Here’s what to look for before your next M12 purchase—and what separates a connector that fits from one that lasts.
Material Choices That Survive Washdowns and Vibration
Stainless steel gets all the attention, but the real workhorse in wet, vibrating environments is often a well-chosen engineered polymer. Materials like acetal and UHMW-PE shrug off repeated hot-water spray and high-pressure detergents without corroding or swelling. They also dampen vibration naturally, which prevents micro-fractures from forming around mounting points. The trick is to match the polymer grade to the specific chemical exposure; a generic nylon part might look fine after a quick rinse, but it can absorb moisture over time and loosen its grip on adjacent components.
When metal is unavoidable, 316 stainless remains the default, but it is not invincible. Chlorinated cleaners and high-velocity spray can still cause pitting on polished surfaces. A better approach is to specify electropolished 316L or, in especially aggressive lines, a duplex stainless that offers higher yield strength. For brackets and guards that see constant oscillation, avoid thin sheet metal; instead, use thicker plate or add stiffening ribs. The added mass may seem counterproductive, but it lowers the natural frequency of the assembly, moving it away from the motor and conveyor frequencies that cause fatigue.
Sealing and joining matter as much as the base material. In washdown zones, exposed threads and crevices gather moisture and bacteria. Use gasketed flanges or welded seams where possible, and back up any bolted joint with a nylon-insert lock nut or a wedge-lock washer. For vibration resistance, look beyond standard rubber mounts. Thermoplastic elastomer isolators hold their spring rate longer than natural rubber and resist degradation from cleaning agents. Combining the right isolator with a material that does not retain water gives you a setup that survives both the hose and the hum.
Certifications That Hold Up Under Audit
Some badges look impressive on a website but fall apart the moment a third party asks for proof. The certifications that actually survive an audit tend to be issued by independent bodies with verified testing methods, not by marketing departments. They come with a paper trail: a certificate number, a published standard, and a clear scope that matches what your business actually does. When an auditor calls, you should be able to hand over the original report without scrambling.
A common mistake is treating certification as a one-time checkbox. Audits have a way of revealing whether the underlying process still matches the initial approval. That means renewal cycles matter more than the logo itself. Certifications with annual surveillance audits or periodic re-testing hold up better because they force the organization to stay honest. If a standard hasn't been revisited in five years and no external review has occurred since, expect uncomfortable questions.
The strongest credentials also spell out what they do not cover. Vague wording like "certified secure" rarely survives scrutiny. What holds up is a precise claim: which systems, which locations, which product lines, and which version of the standard. When the documentation is specific enough to be verified line by line, the certification stops being a decoration and starts functioning as evidence. Under audit pressure, that specificity is the difference between a smooth review and a failed one.
Delivery Commitments You Can Plan Around
When a supplier gives you a date, you build your week around it. That only works if the date actually holds. We treat delivery windows as a promise, not a suggestion, because missed freight has a way of quietly eating into your schedule, your labor costs, and your customer's patience. Every quoted timeline goes through a simple reality check: current order volume, lane history, and driver availability. If something looks tight, we tell you before you find out on the dock.
Most delays don't come from the road. They come from fuzzy handoffs, half-confirmed pickups, and carriers who overcommit. We keep the middle of the process boring on purpose. Pickup confirmations are logged with names and times, not just checkboxes. Route monitoring happens while the truck is moving, so a slowdown in one state doesn't become a surprise at your receiving door four hours later. You get updates that actually change what you can do, not just status ping noise.
The real test of a delivery commitment is what happens when a storm, a breakdown, or a border backlog gets in the way. You'll hear from us before you have to ask. We'll give you a revised window that's grounded in what the driver can actually do, not what looks good in an email. Over time, that reliability shows up in fewer emergency calls, less buffer inventory sitting idle, and a schedule you can defend to your own team without crossing your fingers.
Application Engineers Who Know Your Network Topology
Most vendors hand you a generic troubleshooting script. Our application engineers actually sit down with your network diagrams before the first call. They learn where your core switches live, how your VLANs are segmented, and which links carry the heaviest traffic. That means when something breaks, the conversation starts with your topology already on the table—not with a blank whiteboard and basic questions you have answered a dozen times before.
This familiarity changes the tone of support. Instead of slowly walking through device inventories or guessing at traffic paths, our team jumps straight to the affected segment. They might point out that a route flap on your distribution layer is impacting an application two hops away, or that a misconfigured trunk between two specific buildings is causing intermittent latency. It feels less like explaining your environment to a stranger and more like troubleshooting with a colleague who has been in your server room.
We keep that knowledge current, too. After each change window or infrastructure update, our engineers refresh the topology notes tied to your account. So the next time you reach out, they are not working from stale assumptions. For you, that means fewer repetitive explanations, faster root-cause analysis, and support that treats your network as a specific place rather than a generic case number.
Lot-Level Traceability for Fast Fault Isolation
Lot-level traceability changes how quickly a production line can move from symptom to source. Each lot receives a unique identifier that travels with it through assembly, test, and packaging, carrying links to the exact machine recipes, incoming material batches, and operator shifts involved. When a failure signature appears in the field, engineers can pull that lot's full genealogy and place it alongside other lots built in the same window. The deviation often shows up where the records overlap: a slightly cooler reflow zone, a paste lot past its ideal exposure time, or a test socket with rising contact resistance.
The speed advantage comes from narrowing the search space before any destructive analysis begins. Instead of walking through every possible contributor, the team can focus on conditions shared by failing lots and absent from passing lots. That comparison is what turns traceability data into a diagnostic tool rather than a storage burden. It also supports swift containment because affected units can be identified by lot code, placed on hold, or pulled back from a customer before the issue spreads across multiple shipments.
In high-mix production, this matters even more. A single line might switch between small batches several times per shift, and a gradual tool drift or material contamination can hide inside that variety. Lot-level records make it possible to connect failures that otherwise look random and reveal a common origin, such as one feeder calibration or one supplier sublot. That kind of visibility keeps fault isolation focused on the process instead of leaving it to guesswork and extensive retesting.
Change Notifications Before They Reach Your BOM
Change notifications often arrive as hurried requests that do not account for how a part fits into the larger assembly. Reviewing them before they show up in the bill of materials helps catch outdated part numbers, weak substitutions, and incomplete supplier details while the issue is still easy to fix.
Instead of letting every notification trigger an immediate update, route it through a short validation step. Confirm that the proposed component truly meets form, fit, and function requirements, and check whether the manufacturer data is current. If anything looks off, the request can be returned with a comment before it quietly changes the BOM record.
This keeps the revision history cleaner and gives procurement a clearer signal before inventory decisions are locked in. It also reduces the effort of unwinding dependent changes later, because the original request was already screened for conflicts. Over time, fewer surprises reach production and the BOM stays closer to what engineering actually intends.
FAQ
Look past the catalog. Start with the supplier's understanding of your actual operating environment—vibration, washdowns, thermal cycling—and whether they ask about mating cycles, cable routing, and field assembly before quoting. A supplier that treats M12 as a commodity often misses details that cause intermittent faults later.
The body gets the attention, but contacts determine long-term resistance stability. Solid turned contacts, consistent normal force, and proper plating thickness across the full temperature range matter more than a rugged-looking housing. Marginal contacts can pass a bench test and still fail after months of micro-motion and thermal stress.
Look for UL and IEC compliance plus application-specific approvals if you're in food, rail, or hazardous areas. But treat certifications as a floor, not a differentiator. Ask for the actual test reports behind the marks, especially for shock, vibration, and ingress protection. Some suppliers certify a family while only a few variants are fully proven.
Request a factory audit or at least detailed process data: crimp force monitoring, continuity testing on every assembly, lot traceability for raw materials, and sample retention. A supplier that can show process capability data and not just final inspection results is far more likely to deliver consistent M12 assemblies.
IP67 or IP68 is common, but the rating alone doesn't tell you how the connector behaves under pressure washdown, thermal shock, or repeated mating. Ask about the gasket material, sealing geometry, and what happens after 500 or 1000 cycles—not just the fresh-out-of-box condition.
Yes, often it is. The way a supplier handles overmolding, strain relief, and cable exit angles affects field life. Even if you start with a standard part, you want a supplier that can tune the assembly later without changing the connector platform, because real installations rarely stay standard forever.
Ask for their obsolescence process, minimum product lifecycle commitment, and how they notify customers about material or process changes. Reliable industrial connectivity depends on not having to requalify every two years. A good supplier will have a documented change notification process and keep compatible variants available across design revisions.
Conclusion
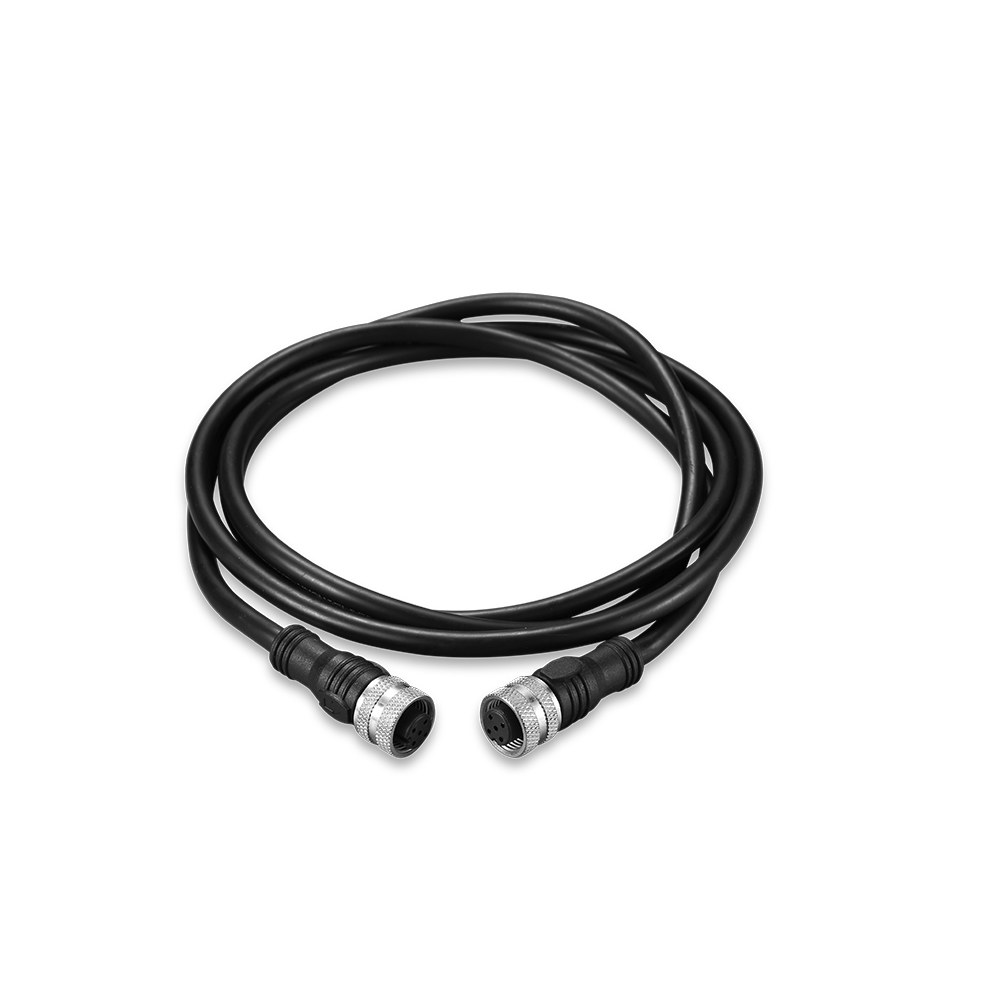
Reliable M12 connectivity starts with suppliers that treat the connector as part of a production environment, not just a catalog item. That means specifying stainless steel or nickel-plated brass housings, Viton or EPDM seals, and potting compounds that stay stable through aggressive washdown cycles and constant low-level vibration. The same practical lens applies to documentation. UL, IEC, and IP ratings should be backed by current test reports rather than logos on a datasheet, because audit teams will ask for traceable evidence. Delivery dates also need to reflect actual capacity. A supplier that quotes the same standard lead time for every part number, whether a standard 4-pin A-coded connector or a custom shielded variant, has not thought through its own constraints.
When a segment drops offline, support depth becomes visible quickly. Application engineers who can discuss topology, cable bend radius, shielding continuity, and IP67 mating behavior save more time than a vendor with a large catalog and a slow helpdesk. Lot-level traceability then shortens downtime. If a specific batch of contacts or overmold compound is linked to an intermittent fault, that data narrows the search instead of forcing a full line audit. Finally, the supplier should flag material or process changes before updated parts arrive in a buyer's BOM, giving design and quality teams enough time to assess fit, function, and regulatory impact.
Contact Us
Contact Person: Hayley Liang
Email: [email protected]
Tel/WhatsApp: +86 13480625451
Website: https://www.reunion-china.com/