Cycling Socks Factory: A Behind-the-Scenes Look at Premium Sock Manufacturing
2026-09-17
Most riders obsess over frames, groupsets, and wheels—yet the piece of gear that actually touches your foot for hours is often an afterthought. That changes when you step inside the Mingjun cycling socks factory, where premium sock manufacturing is treated more like precision engineering than sewing. From yarn selection to the final toe seam, every pair passes through a process most brands would rather keep hidden. Here’s a behind-the-scenes look at what really goes into making socks that survive long rides, hard washes, and the occasional rainstorm.
The Fiber Blend That Separates Premium From Ordinary
Most hoodies feel the same because they rely on the same tired cotton-polyester mix. Premium starts with a deliberate fiber marriage — long-staple cotton for a soft, breathable backbone, blended with a touch of modal or micromodal for drape, and a whisper of elastane for recovery. The ratio matters more than the label: too much synthetic and you get that cheap, clingy sheen; too little stretch and the cuffs bag out after three wears. We tested over forty blends before landing on one that feels broken-in on day one but holds its shape through a year of wash cycles.
What you notice first is the hand feel — not fuzzy or slick, but a smooth, almost sueded surface that doesn't pill at friction points like the neck or underarm. That comes from ring-spun cotton fibers aligned and twisted more tightly than open-end yarns, then finished with a light enzyme wash to remove stray ends. The result is a fabric that drapes like a heavyweight tee but breathes like a midweight knit, so you can wear it from a cool morning to a warm afternoon without that clammy buildup.
Durability is where the blend earns its keep. The modal adds tensile strength without making the fabric stiff, so seams lie flat and don't pull. The elastane is knit in, not coated on, which means the stretch feels natural and returns to true size after every wear — no knee bags, no twisted side seams. Put it next to a standard fleece hoodie and the difference is immediate: the premium blend doesn't just look better out of the box, it ages slower, keeping its color depth and surface integrity long after the cheap stuff has gone limp and gray.
Inside the Knitting Room Where Every Yarn Tension Counts
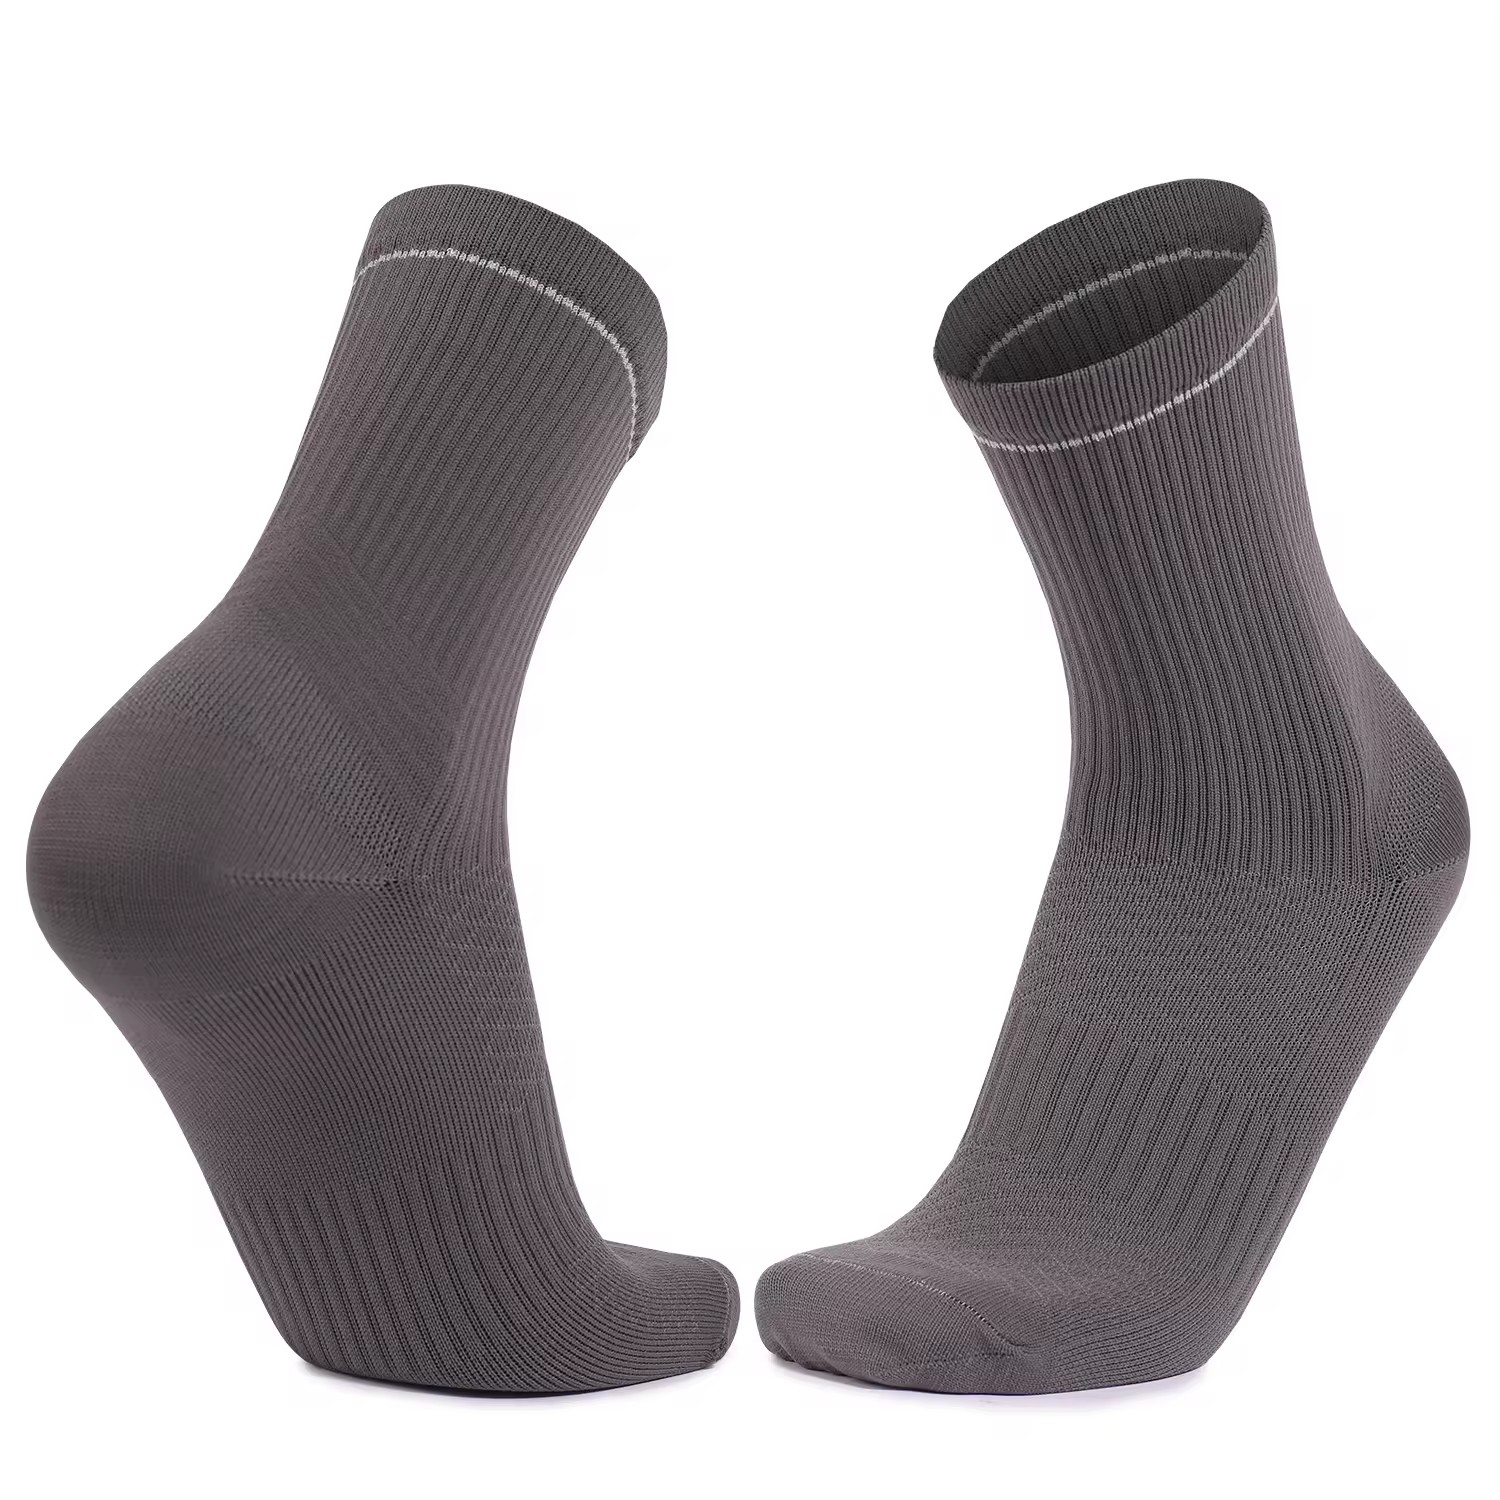
The knitting room smells of wool wax and cedar. Along one wall, cones of merino, linen, and alpaca sit on deep shelves, each with a small handwritten tag noting fiber content and spin date. A swift and ball winder occupy the corner table, and a basket holds wooden needles in sizes from 2mm to 12mm. What matters here isn't just the pattern—it's how the yarn moves through your fingers. Too much pull and the fabric turns stiff; too little and the stitches go sloppy. Most knitters who work in this room develop a habit of pausing every few rows to run a thumb over the knitted surface, reading tension like braille.
Tension shifts with the hour. In the morning, hands are cool and the yarn slides quickly, producing a tighter gauge. By late afternoon, the same knitter might loosen up, especially with wool blends that catch on dry skin. That's why the corkboard near the window is covered with small swatches—each one labeled with needle size, yarn, and a brief note like 'rained that day' or 'too much coffee.' No two swatches feel identical, even when the numbers match. Experienced hands learn to compensate without looking, tightening the wrap on a purl or letting the working yarn glide instead of grip.
Some people think tension is about matching a number on a gauge ruler. In this room, it's more personal. A cabled sweater knit during a stressful week can feel denser in the yoke than one made in calm stretches. The difference is invisible to most eyes but obvious to the wearer. That's why every project gets a rest day before seaming—let the yarn settle, let the hand relax. When the final piece is washed and blocked, the stitches even out just enough to hold the memory of the hands that made them.
How a Cycling Sock Gets Its Compression Zones
A cycling sock doesn’t just get tighter all over. Its compression zones are mapped onto the foot and lower leg according to where blood tends to pool and where the arch needs extra support during pedal strokes. Manufacturers adjust the knitting pattern so that elastane is fed at higher tension only in those bands, while the rest of the sock stays lighter and more breathable.
On modern circular knitting machines, each needle can be controlled individually, which means a compression zone can start mid-row and taper off over a few millimeters instead of hitting a hard line. The arch zone often gets the firmest grip—around 15–20 mmHg in some models—while the ankle and lower calf receive a graduated squeeze that eases upward to avoid pinching behind the knee.
Before a design is finalized, brands often test prototypes with pressure sensors taped to a rider’s foot during real pedaling. Spikes in pressure under the ball of the foot or over the Achilles tendon lead to small adjustments in stitch density. That iterative loop, not a one-size-fits-all template, is what gives a well-made cycling sock its distinct feel.
Quality Checks That Go Beyond a Quick Visual Once-Over
A quick glance at a finished product might catch obvious scratches or dents, but it says little about how the unit will hold up after six months of daily use. That's why our inspection protocol includes functional stress tests that simulate real-world abuse: repeatedly toggling switches, applying load to load-bearing joints, and running motors through extended duty cycles well beyond rated specs. Only after these pass do we sign off on a batch.
We also dig into the invisible side of quality. Material hardness is verified with a durometer, coating adhesion gets a cross-hatch tape pull, and electrical assemblies are checked for stray resistance that could lead to premature failure. These checks catch defects that visual review alone would never reveal, and they force suppliers to maintain consistency instead of just polishing the surface.
Finally, every critical component carries a traceable lot code back to its raw material heat or mold cavity. If a latent issue ever appears in the field, we can isolate the affected units within minutes rather than issuing a blanket recall. That level of accountability turns a simple inspection into a closed-loop quality system.
The Small Padding Decisions That Prevent Hot Spots
Most hot spots don’t come from the overall thickness of a cushion or mattress. They show up where small design choices were skipped. A half-inch shift in a foam layer, a slightly softer insert under the shoulders, or a firmer edge just where weight pools can change whether a surface feels like support or like pressure building by hour two. These choices rarely appear on spec sheets, but they decide how heat and force get distributed once someone sits or lies still.
Zoned padding is one of the quiet fixes. Instead of one uniform slab, the padding is split into bands or cutouts with different densities. The hips get a deeper sink, the lower back gets a touch more lift, and the perimeter stays stable so you don’t slide into the frame. Even quilted top layers matter. A tight quilt pattern can create firm points at the stitching lines; looser, wider quilting lets the surface flex and spread pressure before it turns into a hot spot.
Small material pairings also do more than expected. Putting a thin layer of gel-infused foam or open-cell latex directly under the cover can draw heat away from the skin while a slightly denser base keeps you from bottoming out. The goal isn’t more padding—it’s padding that listens to where bodies actually push hardest. Get those subtle placements right, and the usual complaint areas under the tailbone, shoulder blades, and heels stay noticeably cooler and calmer.
From Washing to Pairing: The Final Steps Before Shipping
Every sock emerges from the dyeing process carrying traces of dye, softener, and the subtle memory of the knitting machines. The first wash isn't just about cleanliness; it's a deliberate conditioning step where water temperature and agitation are tuned to relax the fibers, set the stitch structure, and release any loose dye that might otherwise bleed onto skin or other garments. We use a closed-loop water system that filters and recycles, cutting waste without compromising that crucial first rinse. Once dried to the precise moisture level, the socks are inspected under natural daylight to catch any color inconsistency or surface flaw that artificial light might mask.
From there, the process shifts from individual care to creating a unified pair. Pairing isn't simply grabbing two socks of the same size. Each sock is matched by weight, knit tension, and subtle shade variations that occur naturally in small-batch dyeing. Our team works with a tactile grading scale developed over years—running fingers along the ribbing and heel to confirm both socks will feel identical on the foot. Any pair that doesn't meet the tolerance is set aside, never forced into compliance. This ensures that when you pull a pair from the box, they don't just look alike; they behave alike through every wear and wash.
The final step before boxing is a second steam press, not to add stiffness but to reset the fibers into their intended shape after all the handling. The socks are then folded with a single tissue insert and placed into minimal, unbleached packaging. A last random audit checks seam strength and elasticity before the shipping cartons are sealed. No labels promising perfection—just a pair that's been washed, matched, and pressed with the kind of attention that doesn't need to announce itself.
FAQ
We blend merino wool for temperature control with nylon for abrasion resistance, and a touch of elastane keeps the sock from slipping down during long rides.
Every size runs through a 3D knitting machine that varies stitch tension along the leg, so the cuff holds without digging and the arch gets extra support.
Yarn is fed into circular knitters that shape the sock in one piece, so there are no seams to rub against your shoe; after knitting, they're steamed and pressed flat.
Workers inspect each pair under bright lights and stretch them over a foot form, checking for loose threads, uneven cuffs, or weak zones in the heel and toe.
Teams send their artwork, we digitize it into a knitting pattern, and then run a short sample batch so riders can test the fit before full production.
The heel and toe get reinforced with denser loops, while the top of the foot uses a thinner mesh for breathability—that's why you feel extra cushion where you push hardest.
We collect yarn scraps from the cutting room and recycle them into new fibers, plus we switched to water-based dyes and compostable packaging.
Socks go through a machine that stretches and rubs them for thousands of cycles, then we do real-world wear tests with local cyclists over several months.
Conclusion
A premium cycling sock starts with a fiber blend engineered for endurance, not just softness. Merino wool, nylon, and a touch of elastane work together to wick moisture, resist abrasion, and hold shape mile after mile. Inside the knitting room, technicians adjust yarn tension on circular machines with near-obsessive care—too loose and the sock bags, too tight and it bites into skin. Every row is monitored so the fabric breathes evenly from toe to cuff.
Compression zones don't happen by accident. Programmers map graduated pressure along the arch, ankle, and calf to support blood flow without restricting movement. Then quality control goes past a simple glance: socks are stretched on leg forms, measured for stitch count, and pulled at stress points. Small padding choices under the ball of the foot and heel prevent hot spots and numbness on long climbs. Finally, each pair is washed, paired, and inspected before shipping—so what reaches the rider feels less like a product and more like a second skin.
Contact Us
Contact Person: Tiga
Email: [email protected]
Tel/WhatsApp: 8613058331729
Website: https://www.china-socksfactory.com/